 Skip to content
Heavy-Duty Performance: Industrial Warehouse Floor Coating in Central Jersey
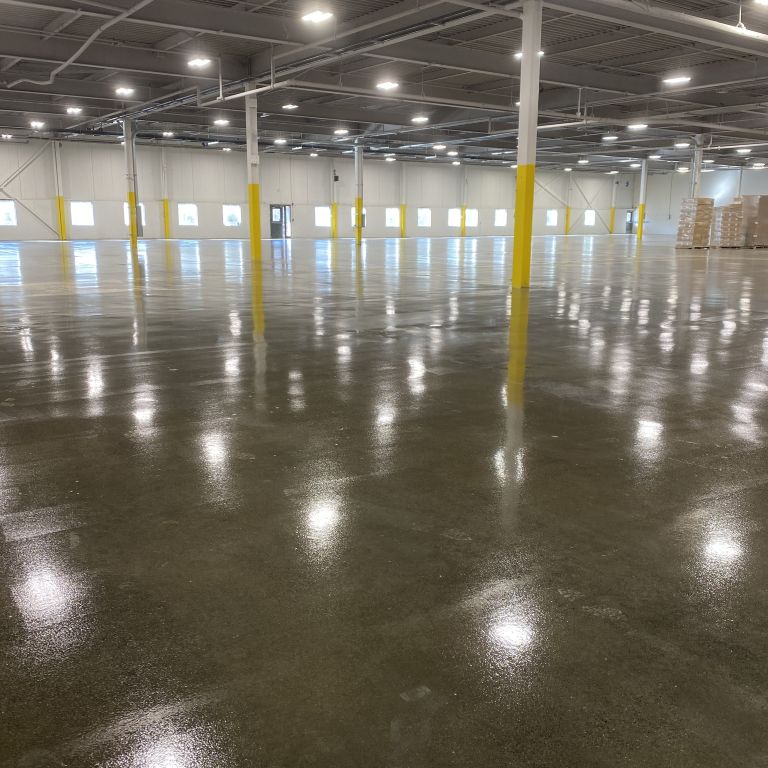
Industrial warehouse floor coating systems are essential for protecting the concrete foundations driving Middlesex County and Central Jersey’s massive logistics, manufacturing, and supply chain networks. From bustling distribution hubs to high-traffic manufacturing plants, your facility’s foundation literally takes a beating every single day. If your concrete floors are dusting, cracking, or showing signs of intense wear, it’s time to invest in a commercial-grade solution.
Choosing the right warehouse floor coating is the single best way to protect your infrastructure, improve employee safety, and optimize your daily operations.
We provide comprehensive flooring coverage across the region. Read about our latest projects delivering heavy-duty industrial warehouse floor coating in Central Jersey to see how we protect high-traffic logistics hubs.

The Powerhouse Corridors of Central Jersey
We specialize in transforming facility floors across Middlesex County and the surrounding regions, focusing heavily on the areas driving New Jersey’s commercial boom:
Cranbury (Exit 8A Corridor):
As one of the nation’s most prominent logistics hubs, the Exit 8A corridor requires floors that can withstand constant, heavy-duty forklift traffic and 24/7 fleet operations.
Woodbridge & Perth Amboy:
Located near major ports and highways, warehouses in these areas handle massive shipping volumes and chemical exposure, requiring highly resilient, chemical-resistant surfaces.
South Brunswick / Dayton:
From pharmaceutical storage to e-commerce fulfillment, facilities here rely on pristine, dust-free environments to maintain strict quality control standards.

Why Your Facility Needs an Warehouse Floor Coating
Standard concrete simply isn’t built to handle the rigorous demands of modern supply chains. Over time, bare concrete degrades, creating fine dust that settles on your inventory and machinery.
Applying an warehouse floor coating creates an impenetrable barrier that seals your concrete. This advanced coating system prevents moisture infiltration, resists aggressive chemical spills, and easily bears the load of heavy machinery and high-capacity shelving units.
Additionally, ensuring absolute durability under heavy machinery. Learn more about our specialized industrial warehouse floor coating options for manufacturing plants in Middlesex County.
This advanced coating system prevents moisture infiltration and resists aggressive chemical spills. For more technical specifications on chemical resistance, check out our Epoxy Flooring FAQ.
Unmatched Durability for High-Traffic Hubs
Every hour of downtime costs your business money. That’s why our industrial warehouse floor coating systems are engineered for rapid installation and long-term durability. We utilize premium epoxies, polyaspartics, and urethane cements designed to cure quickly, allowing you to get your operations back online with minimal disruption.
Whether you are managing a massive fulfillment center in Cranbury or a manufacturing plant in Perth Amboy, our floors deliver a seamless, high-gloss finish that actually increases ambient light visibility across your facility floor.

FAQ
For high-traffic Central Jersey logistics hubs handling constant forklift and pallet jack traffic, a urethane cement or a heavy-duty solid-epoxy system with a polyaspartic topcoat is highly recommended. These systems offer superior impact resistance, high compressive strength, and will not gouge or delaminate under extreme structural loads.
Minimizing downtime is our priority. A typical installation can take anywhere from 2 to 4 days depending on the concrete surface preparation required (such as diamond grinding or shot blasting). By utilizing rapid-curing polyaspartic topcoats, we can often have your floor ready for light foot traffic within 24 hours and heavy forklift traffic within 48 to 72 hours.
Yes, absolutely. A professional coating dramatically improves facility safety. We can integrate permanent, high-visibility line striping and safety yellow zone markings directly into the floor system to clearly define pedestrian walkways, forklift lanes, and hazardous areas. Additionally, custom anti-slip textures can be embedded into the topcoat to prevent slip-and-fall accidents.
Proper surface preparation is the most critical step for a lasting bond. We use heavy, industrial planetary diamond grinders and dustless shot-blasting equipment to remove old coatings, oil contaminants, and damaged top layers of concrete. This process achieves the exact Concrete Surface Profile (CSP) required for the resinous materials to fuse permanently with the substrate.
Yes. Bare concrete naturally breaks down over time, creating fine silica dust that settles on inventory, sensitive machinery, and electronic components. An industrial warehouse floor coating completely seals the porous concrete substrate, eliminating dusting entirely and creating a seamless, easy-to-clean surface that protects your products and your workforce.